Search the whole station
Wenzhou Feilong Polyurethane Equipment Engineering Co., Ltd.
Chinese website: http://www.pumcn.com/
English website: https://www.flpumachine.com/
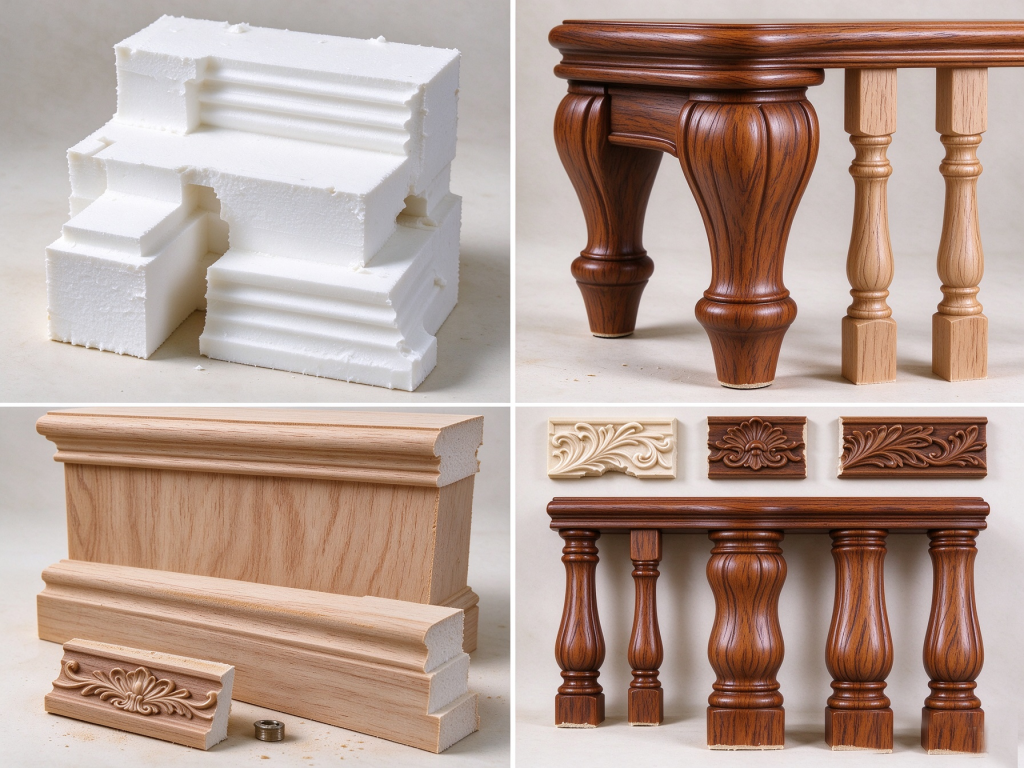
Tree protection is one of the most important issues in environment protection, the self-skinning polyurethane rigid foam is an ideal material in synthetic wood already developed.
1. Comparison of property of synthetic wood:
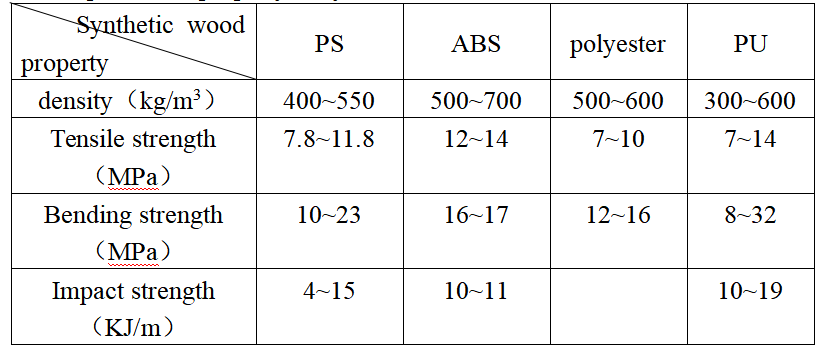
Note: PS:polystyrene
PU:self-skinning polyurethane rigid foam
ABS:acrylonitrile——butadiene——styrene copolymer
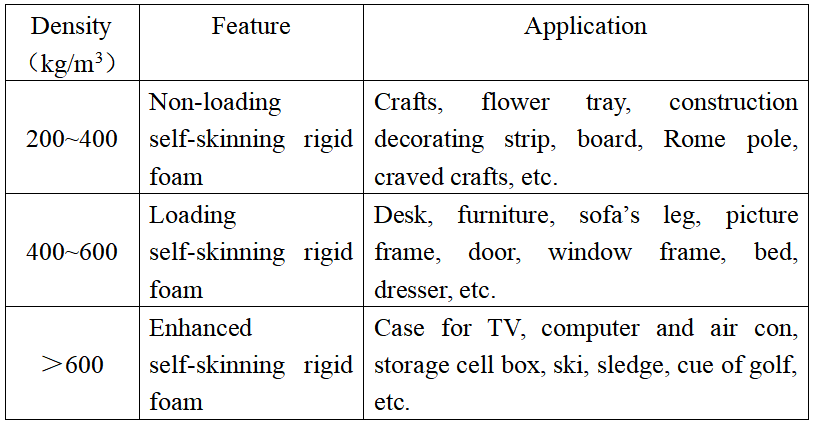
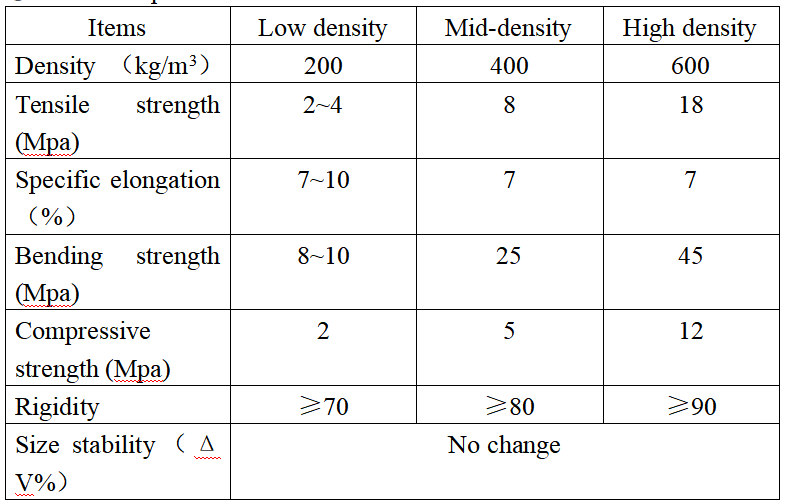
2.Classification of self-skinning polyurethane rigid foam:
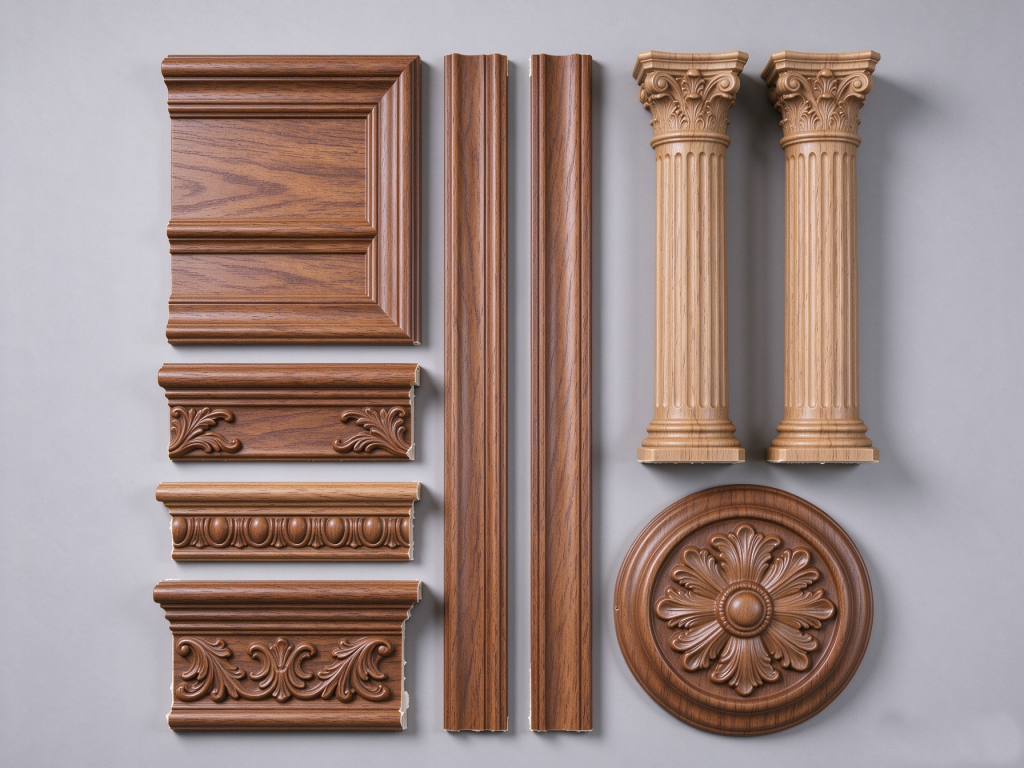
3. Advantages of polyurethane imitated woodwork:
(1)With high strength and light weight, can bear heavy load. It can substitute plasterboard, polyester, fiberglass-reinforced plastics and other synthetic wood, and can used for decorating strip, ceiling, pattern board for droplight, etc. The coping of main gymnasium of Beijing Olympic Game in 2008 is made of polyurethane imitated-woodwork.
(2)The production repeatability of PU synthetic wood is good, the size of product is accurate, the copied pattern is clear, the texture is vivid, and it can replicate every kinds of crafts, and also save labour.
(3)The product is light weight and non-deform, easy to paint color, antiwear, shockproof, insect-resistant and corrosionproof.
(4)It can fulfill mass production, the process is simple and with high efficiency.
(5)The appearance resemble nature wood, and can be processed with traditional woodwork such as drill, plane, saw, nail and stick.
The two purposes for customer purchasing the equipment: one is with high rate of quality product (gain good economic return) and the other is low failure rate of equipment (ensuring normal work.
1. These four factors affect the rate of quality product: material, machine, molder and operation method.
(1)Material: qualified raw material and technics:
At present, the high quality PU imitated woodwork in Yantai, Shanghai, Luoyang, Changzhou and Shaoxin all meet the requirements of customer. The high quality PU imitated woodwork can be produced only follow the requirements such as blending rate, temperature of material and molder.
The reference information for raw material:
(2)Good performance and reliable equipment consisted of two parts:
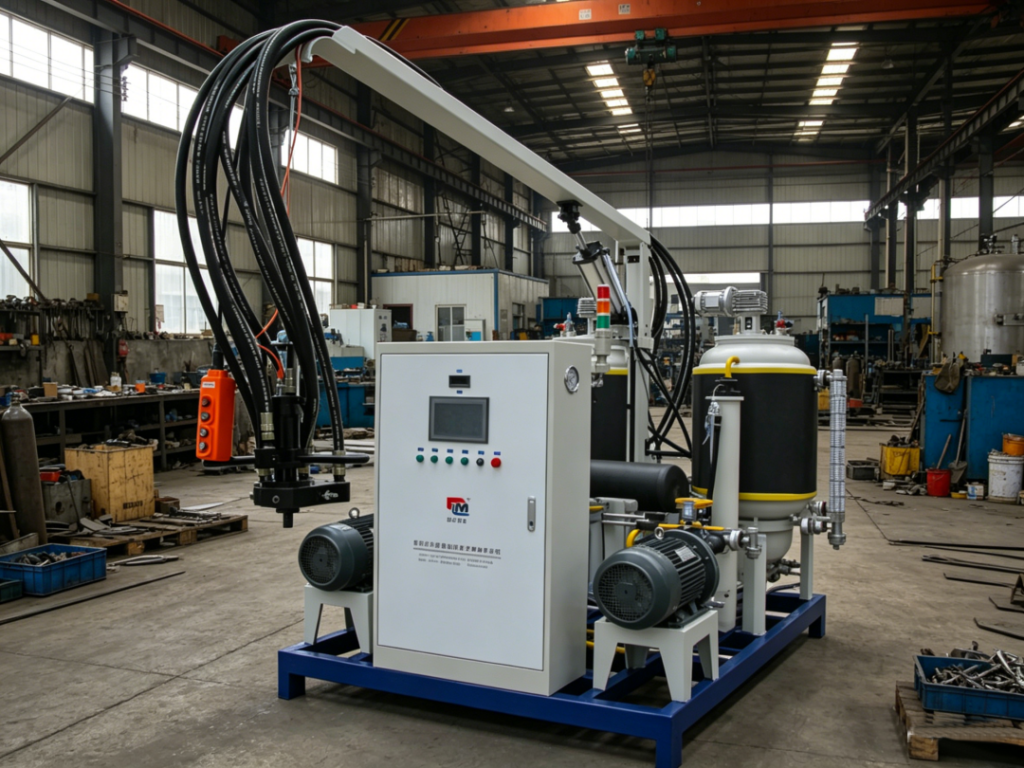
a:Cast-type foaming machine (series PU20F-YA): The two group of primary liquids with certain temperature measure accurately according to the requirement of compounding formula and blend evenly, then cast into molder, and it will generate chemical reaction, so the measurement accuracy and even blending is key factors for high rate of quality product.
b:Molder loading production line: it is usually in long circle shape and consisted of transmission unit, trolley and drying tunnel (driven by step motor).
(3)Reasonable designed molder: applying open-mold or close-mold casting according to the shape and requirement of product and design the molder.
(4)The correct operation procedure. Apply correct casting process (including casting volume, casting time, etc.), and make the casting material filled into molder with layer-flow state. Analyze and clear any malfunction when it occurred.
2. How to reduce the failure rate equipment
(1) The equipment should match with the requirement of raw materials
a:Technical parameters:
b:Composite material
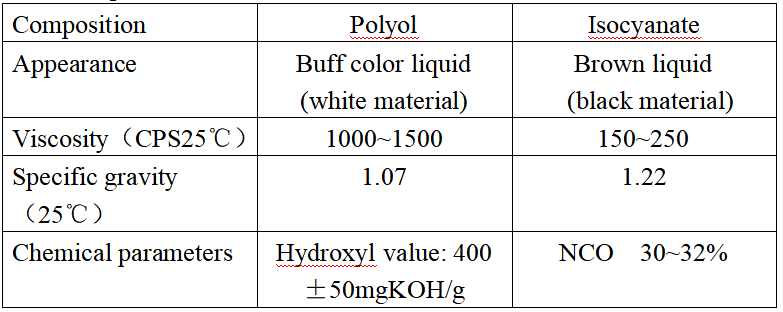
c:Working condition: blending rate (W) A:B=100:100-110.
Temperature of material A: 20±2℃, material B: 25±2℃.
d:Reactivity:
milk white period (CT): 35-40S; initial foaming period (RT): 40-50S
non-cohesion period (GT): 90-100S; demolding period (DMT): 5-6min
e: Features and purposes: This product has features such as high strength, low density, good physical performance, with glabrous surface, non-sopping, sunproof, oil resistant, chemical resistant, insect resistant, non-aging with long time service and non-deforming, its property is superior to wood. The product can process with sticking and pre-burying, and with good decorative property, the forming process is simple by use casting machine.
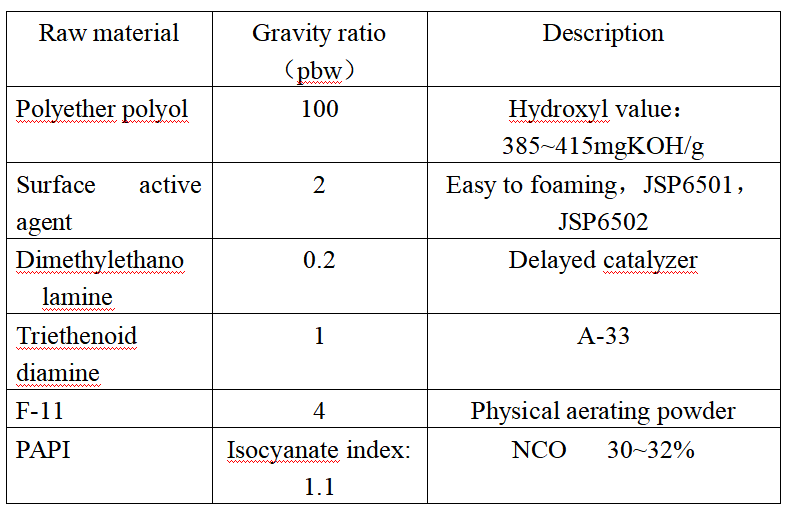
f:Reference compounding formula:
(2) Advanced machine, reasonable configuration, simple structure, good quality of material, convenient operation and maintenance.
(3) The operator or maintenance technician should regularly maintain machine and change failure parts.
3:Flow chart for work process:
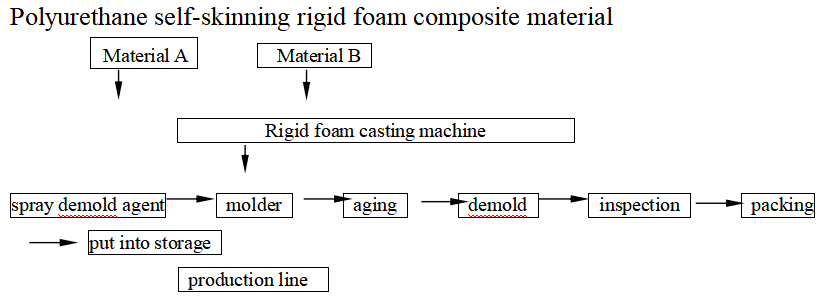
To improve yield and save raw material, the machine interrupted cast the molder on the production line (the casting volume is controlled by computerized controller), after casting a batch of molder, then automatically clean the blending cavity, so it can simultaneously produce several PU bobbers with same or different specification.
(Ⅰ) Rigid foam casting machine (consisted of tank, bump, head and control part). (Details please refer to Flow Chart of PU20F-YA.)
(A). Material tank (tank): the tank is made of acid-resistance stainless steel (argon arc welding), the heating layer and outer are covered with polyurethane rigid foam layer, the new designed structure apply plain lid processed by machine tool, which enhanced the concentricity compare to convex lid, and shorten the blending shaft to make blending more stable and more sealed. As reduce the space on the top of material tank, so decrease the moisture inside the tank which will cause deterioration of raw material.
(B). Measuring parts (pump):
1. The factors affect the measuring precision:
(1) Evenly material feeding and normally filter: the viscosity of primary liquid is pertinent to the material temperature. If the technics is permitted, the material temperature should increase to decrease the viscosity and make the material feeding more convenient. If the viscosity of primary liquid is too high (over 2000CPS), then can add nitrogen gas (<0.03Mpa) into the material tank, so can feed material evenly into measuring pump.
(2) Measuring pump: the driving device, measuring pump and digit display for revolving speed. By applying low speed high precision measuring pump, driven by stepless motor, digit display for revolving speed, the error should less than ±0.5% under normal situation.
(3) The resistance is stable both in material feeding and backflow system, and the pressure adjustment is sensitive.
Note: The measuring method of high performance polyurethane equipments all apply “full-backflow—casting” process rather than “direct-through” process. The “direct-through” process shows as below: The primary liquids A and B after filter will send to blending unit respectively through the measuring pump, then casting after blend evenly.
The advantage of this process is simple operation, no need of backflow pipe, and it is mainly used for those situations with usual requirement such as polyurethane rigid foam spraying.
The “full-back—casting” process shows as below: the A and B primary liquids send to blending unit through measuring pump and controlled by simultaneous switch, both A and B will totally send into the blending cavity then blend evenly by the blender with high revolving speed and are ready to cast. If stop casting, cut off A and B to enter into blending cavity and those will backflow into the original tanks. By regulating the pressure of material-feeding and backflow pressure, it will keep invariable blending rate during casting, so can prevent the change of blending rate when start or stop blending and avoid producing under quality product, so can improve the rate of quality product.
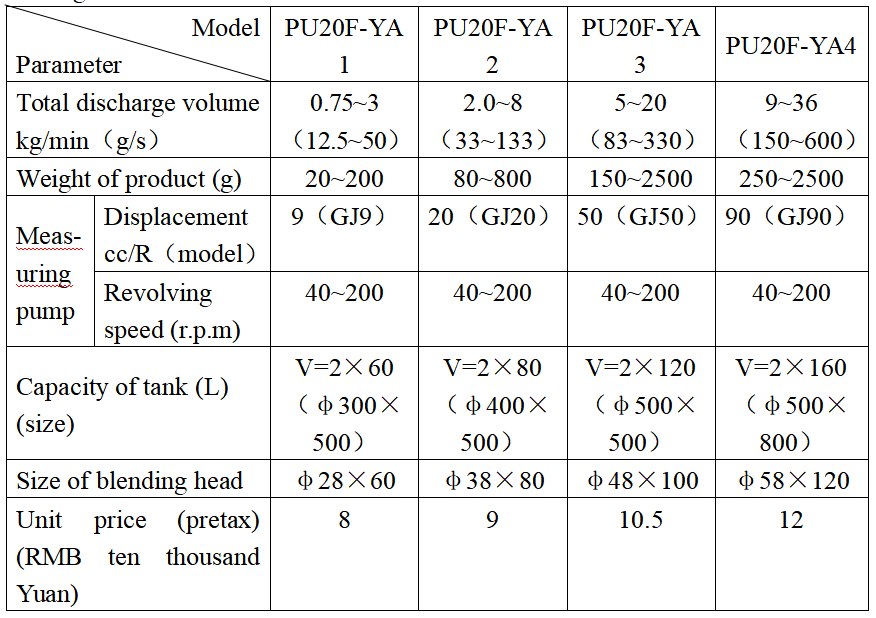
2. Setting and main parameters of measuring pump:
Designed blend rate: A : B=100 : 100~110
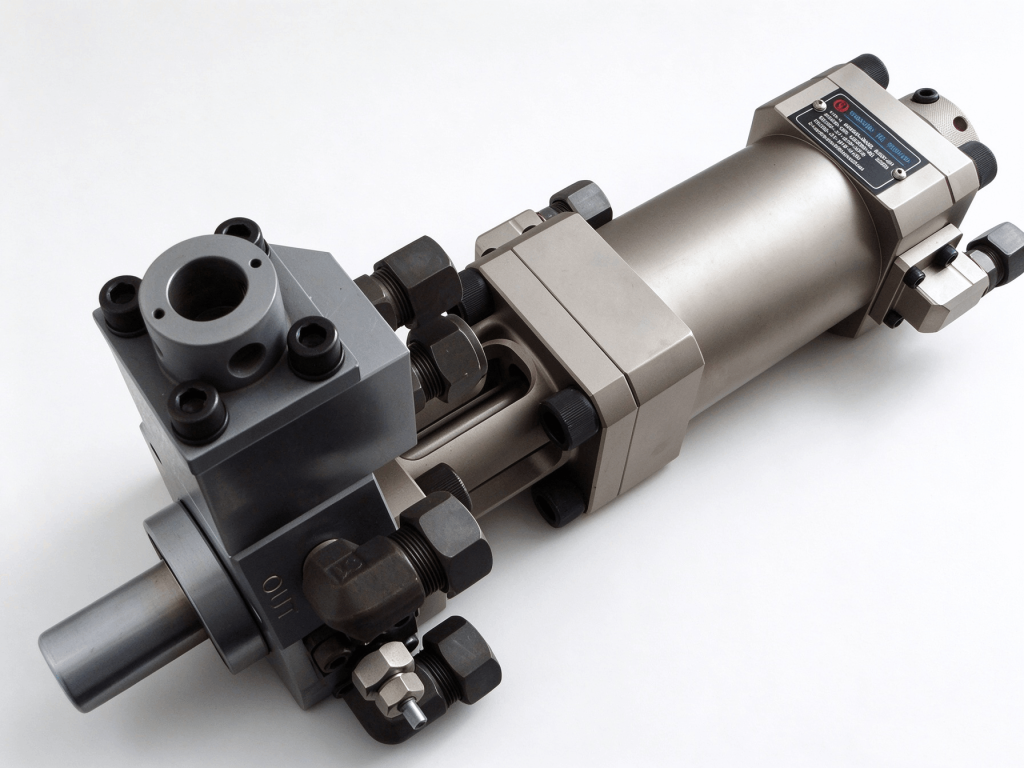
C. Blending unit (blending head)
1.Casting—backflow switch mechanics:
The three-cylinder simultaneously switch two groups rotary valve through rack bar and gear (when the rack bar is on the upper position, the rotary valves A and B will be on air blast or cleaning state, and materials A and B are under backflow state; when the rack bar is on the middle position, the materials A and B are under backflow state, the air blast or cleaning will stop, (so the cleaning hole will not blocked); when the rack bar is on the lowest position, the air blast or cleaning will stop, materials A and B are under casting state, during casting, primary liquids A and B will enter into blending cavity, during backflow, the primary liquids will return back into the respective tank through backflow regulating valve.
2.Pressure adjustment mechanics:
The backflow-regulating valve mounted on the two side of blending head will finely adjust the backflow pressure of primary liquid (the adjustment should be sensitive and with reliable fine adjustment, and should not block).
The casting pressure is regulated by the hole diameter of throttle flake, the hole diameter is decided by this formula: d(mm)=5√Q/V .
Q: flow quantity of primary liquid (L/min), according to the casting volume. V: velocity of flow of primary liquid (m/s), usually be 3-5.
3.Blending transmission and seal of end of shaft:
Two-polarity motor transmitted with lobed belt, the blending speed is 6000 r/m, using imported high-precision bearing, the shaft has precise oil-seal and special seal to prevent the blending material from upward pouring of material. (During operation, the hopper should be changed when the discharge hole of it become small due to material clumping, so can prevent from upward pouring of material result from overpressure in blending cavity.)
4.Cleaning mechanics:
This mechanics is used to keep the blending cavity clean after casting every batch of products (no gas leakage and no cleaning liquid remained) and ensure next casting process can be performed smoothly. Controlled by computerized controller to make it automatically air blast or liquid-cleaning through electromagnetic valve, and it can effectively prevent the primary liquid from enter into cleaning tube.
5.Blending head:
Apply highshear blending head with special design, simple and practical, blend evenly, and will not cause fluctuation of pressure during interrupted casting, easy to clean.
The stay time of blended material in the blending cavity can be adjusted by change the discharge hole of hopper.
D. Controller: control and display
1. Computerized controller (with stable performance, reliable structure, easy operation and learning)
(1)The casting volume can controlled and displayed automatically, and can control 99 work positions with same or different casting volume (casting time:0.10-99.9s).
(2)Control the interrupted casting: after casting, the rack bar of rotary valve should be on middle position (primary liquid backflow and cleaning stop) to prevent the casting head from dropping material, then the motor of blending head stop.
(3)Control automatically air blast and liquid-clean: after casting a batch of molder, if the uncasting time is too long (over 2/3 of milk white period), it should start the automatic cleaning process: air blast—liquid-clean—air blast (the blending head is revolving with high speed during these processes)—air blast (the blending head stop revolving), the blending cavity can be clean and blow dry by adjusting the process time.
2. Temperature control system:
The temperature of material should keep stable, usually the temperature should be 22±2℃, the electric heat tube in the sheath under material tank heat up primary liquid through heating oil, the digit display temperature controller will automatically control the temperature of material through the temperature sensor under the material tank.
3. Pressure display for primary liquid:
Apply high precision digit display pressure meter and thin-film pressure sensor, the precision reaches 0.01Mpa.
4. Flow quantity (revolving speed of measuring pump) display:
Display the measuring value by high precision revolving speed meter, can calculate or measure out the flow quantity and blending rate of every pump.
(Ⅱ) Production line (loop transmission belt and drying tunnel):
1. Transmission unit: the electromagnetic speed-adjustable motor drive the big chain wheel through V-belt and worm wheel, and drag every trolley to move with required linear speed, the other end of loop transmission belt has a tension chain wheel, pull tensely the chain by helix mechanics, the linear speed should be 1.5-15m/min.
2. The trolley and slideway: the production line has 40 trolleys (400×500), every trolley can mount a molder and move on the slideway, the chain beside the trolley will drive it, the slideway wheel mounted on the pedestal.
3. Drying tunnel: on the one side of loop transmission belt has 10 meters long drying tunnel, the trolley and molder will go through it, the wall and top-lid of drying tunnel has heat insulation layer, and the drying tunnel heat up by far infrared, the temperature in the drying tunnel is controlled by temperature controller.
4.Control cabinet: the speed control for loop transmission belt and temperature regulation for drying tunnel, it is convenient to operate.
1.Mold-plastic polyurethane production line has three types of equipments and related technics:
(1)High pressure machine: measured by high-lift pump (>10Mpa), two primary liquids collided with high speed (>150m/s) and blend evenly, after casting, it will turn back to backflow state, the high pressure pusher will clean the blending cavity, its advantage is: the casting head is compact and light weight, no need of cleaning after casting, and it is suitable for those with large casting volume or the long interval between casting (e.g. produce the refrigerator), this machine has complicated structure, high precision of fabrication and installment, still with large investment, the operation and maintenance is difficult. This machine isn’t suitable for those with small total discharge volume, or the blending rate and viscosity of two groups of materials are different with largely, or any primary liquid with loading material.
(2)High speed machine: measured by mid-pressure high precision measuring pump, blended by indent screw stem with high revolving speed (>15000rpm), scrape the blending cavity by conic high speed screw stem, so no need of use or use less solvent to clean (e.g. DESMA machine), the precision of fabricating and installment are very high, and with complicated structure, high level of automation and large investment on equipment, still also, the operation and maintenance are difficult. This machine is mainly used for those with small total discharge volume.
(3)Low pressure machine: measured by low pressure (<0.5Mpa), low speed (n<300rpm), high precision measuring pump, blended evenly by mid-speed (n=4000-8000rpm) mechamics, it should be clean after casting a batch of products. The advantage of this machine is: with reasonable structure, save investment, the operate and maintenance are easy, and suitable for those primary liquids with different viscosity and blending rate, work reliably when the temperature is high or added loading material, still with large range of adjustment and good adaptability, and can fulfill multi-function with one machine (e.g. it can produce not only the foamed product, such as flexible foam, rigid foam and semi-rigid foam, but also polyurethane elastomer which is no air bubble). With several decade’s experience and technical improvement in this high performance low pressure machine in our country, by now, the performance of it reaches the advanced level in the same line of imported equipment.
2. The comparison of these three types of machine:
Even through the high pressure machine or high speed machine has its advantages, for reliable performance, it is still rely on imported machine or assembled by imported parts, and its price is 5-10 times of low pressure. As a developing country, we cannot afford these equipments, and also our clients can gain less economic return from it. More over, the industry is comparative weak in our country, esp. the material, heat treatment and fine process are lagged behind the developed country. Even though the homemade high pressure machine or high speed machine has been produced, the quality and performance of it is still inferior to imported machine, e.g. the serial GZ and GF high pressure foaming machine made by Wenzhou Yuecheng Chemical Equipment Factory in 1994 (details please refer to “Polyurethane Foamed Plastic” Version 2, P994), ten years pasted, yet the technology still have not broken through, so cannot be widely used in industry. As for polyurethane sole forming machine, the high speed or high pressure machine has been produced for a long time abroad, yet it cannot be widely used for low efficiency, low rate of quality product and large investment, difficulty in operation and maintenance. For steering wheel and handrail for automobile and other self-skinning product, it is best to produce by high pressure machine, but now, with experience and technical improvement, the quality and rate of quality product of the closed-mold self-skinning product produced by low pressure machine are not inferior to those produced by high pressure machine, yet the investment decrease largely, e.g. the large rigid foamed product which formerly produced by high pressure machine, by now, a number of enterprises produce large polyurethane rigid foamed laminated board by low pressure machine, and gained good economic return with perfect quality and low cost.
Ⅴ. The quality of product carry out “three guarantees”, the guarantee period is one year. The supplier should dispatch technician to install and adjust the equipment after it deliver to the customer.
Terms of payment: prepay 30% of total value when the contract take effect, pay another 65% when pick up the goods, and pay off the remaining amount after installment and adjustment and pass the test. The packing cost is borne by the supplier, the delivery cost is borne by the customer.
 FEILONG PU MACHINE