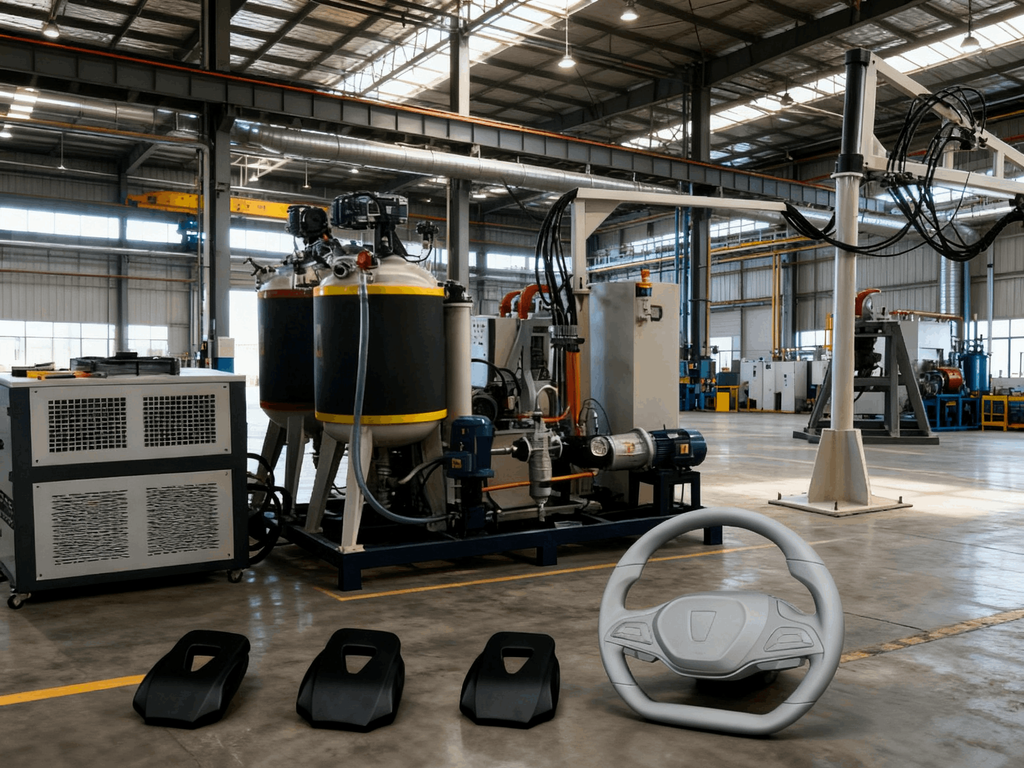
(Image: Feilong Polyurethane Equipment – Self Forming Foam Machine) Ⅰ、 A requirement Feilong Polyurethane Machinery Equipment has successfully developed a complete set of production equipment for polyurethane self skinning products (steering wheels, handrails, etc.) since 2001. After years of continuous improvement and refinement, its main performance has reached the level of similar imported equipment, and it can be used for different raw materials to produce various specifications, requirements, and uses of self skinning products (steering wheels, handrails, etc.). Domestic equipment has the following advantages over imported equipment: 1. Tailored according to user requirements, efficient and practical equipment that meets process conditions, creating abundant benefits for users. 2. Timely and effective after-sales service to solve various problems encountered by users on time. 3. Long term provision of cheap and high-quality accessories, without causing “affordability but inability to maintain” due to the use of imported equipment and high accessory prices, resulting in high maintenance costs and a significant increase in production costs. 4. Domestic equipment has lower costs, and when choosing domestic equipment that is comparable to imported equipment, both investment and maintenance costs can be greatly saved.
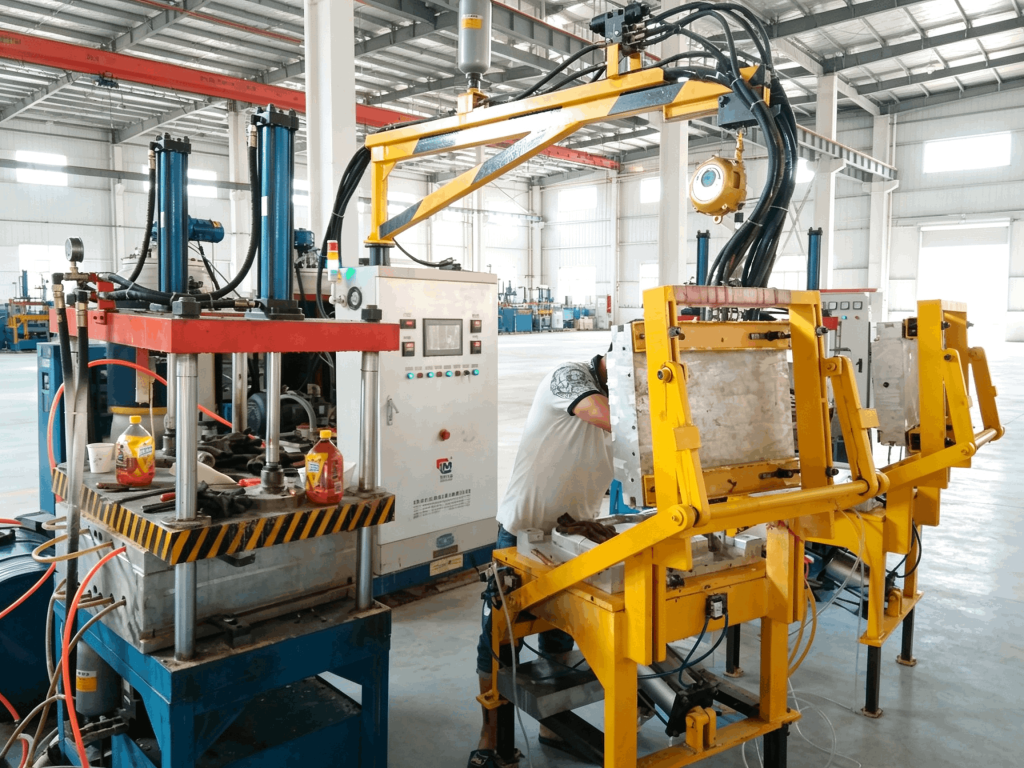
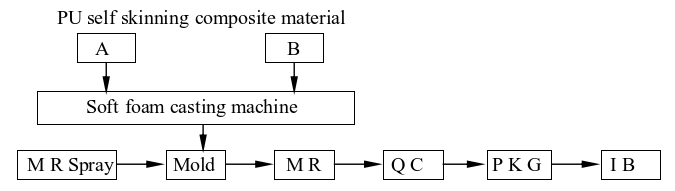
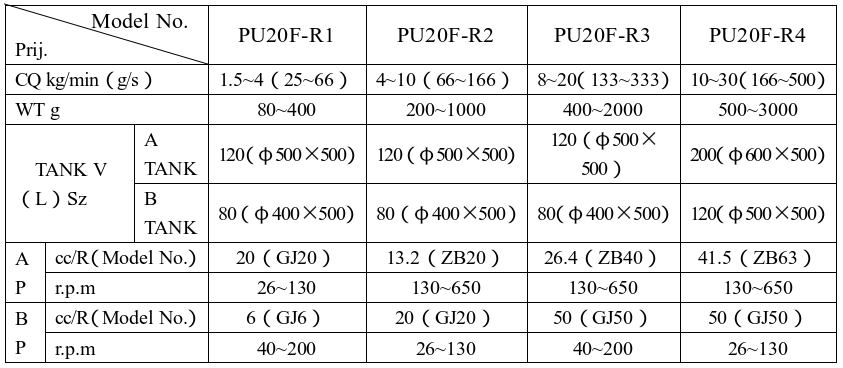
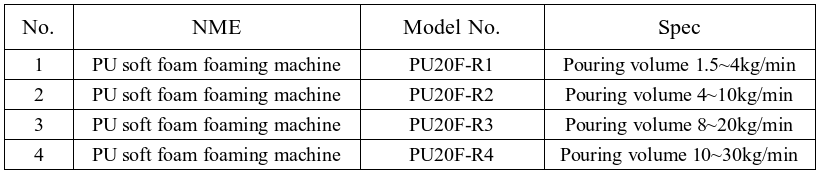
(Image: Feilong Polyurethane Equipment – Foaming Machine PU20F) Ⅱ、 Two purposes: Users hope to achieve two goals when purchasing equipment: high authenticity rate (to achieve substantial benefits) and low failure rate (to ensure normal production) 1. How to achieve the highest genuine product rate: (materials, machines, molds, usage) (1) Qualified raw materials and suitable processes: At present, excellent units such as Yantai Wanhua, Wenling Defeng, and Shanghai Bi can all supply high-quality polyurethane self skinning composite materials. As long as the required mixing ratio, material temperature, and mold temperature are met, it is possible to produce high-quality self skinning products. Basic requirements for polyurethane self skinning products: ① It must have a self bonding layer with a certain strength, thickness, and smooth surface. ② The core and skin have a significant density difference, and the core should have a highly elastic perforated structure. ③ Its main mechanical properties: Forming density 400-600 (kg/m3) Skin hardness 4085 (Shore A) Skin density/foam core density (kg/m3) 8001100/150400 Skin tear strength/foam tensile strength (N/mm2) 312/0.31.5 Elongation at break/elongation at break of foam core (%) 100200/80~160 ④ Adjusting different mixing ratios or compositions can produce self skinning products with different surface hardness or elasticity. (2) Equipment with superior performance can ensure long-term reliable operation: The equipment for producing polyurethane self skinning products mainly consists of two parts: ① Pouring type foaming machine (PU20F-R): Two components of raw liquid controlled to a certain temperature are accurately measured and uniformly mixed according to the formula requirements, and then quantitatively poured into the mold. As the production of polyurethane self skinning products is a chemical reaction, accurate measurement and uniform mixing must be achieved, which is the key to ensuring the product yield. ② The mold carrying production line (designed according to production requirements) is generally circular or elongated to accommodate multiple molds. (3) Reasonably designed molds are beneficial for the smooth flow of castables and the elimination of surface bubbles: When pouring in a closed mold, the high demand self bonding surface should face downwards, and the pouring material should enter the mold cavity in a thin film shape. In order to eliminate the introduction of bubbles in the material, the flow rate should be ≤ 1.5m/s, the gate thickness should be ≤ 2mm, and the upper and lower molds should be tightly adhered, allowing for exhaust without material leakage. (4) Correct operating method: Able to use appropriate pouring processes (pouring amount, pouring time, etc.) according to different molds. When abnormal phenomena occur, able to analyze them specifically and quickly eliminate them. 2. How to minimize equipment failure rate: (1) The selected equipment can adapt to the raw materials used (meet the required process conditions) ① Common parameters: Weight mixing ratio A: B=100:4045 Material temperature: 22 ± 2 ℃ Mold temperature: 3545 ℃ Material A: (polyether polyol component) Viscosity: (25 ℃ mpas) 800-1200 Specific gravity: (25 ℃) 1.05-1.08 B material: (isocyanate component) Viscosity: (25 ℃ mpas) 200-600 Specific gravity: (25 ℃) 1.2-1.24 ② Reactivity: Milk white period (CT): 12-20 seconds Rising period (RT): 60-120 seconds Gelation period (non stick period) (GT) 40-80s Demoulding period (DMT): 180-300S (3-6 minutes) ③ Process requirements: a、 Self structuring foaming should strictly control the water content in the raw materials, as H2O reacts with NCO to generate CO2, which is difficult to exist in liquid form in the foaming system, thus disrupting the formation of the skin. Generally, H2O in polyols is required to be less than 0.01%. b、 To obtain a certain thickness of skin, an excessive amount of mold should be injected (usually 20-40% excess), and increasing the amount of foaming agent can increase the density of the skin; If you want to produce thin leather products, you can adjust it by reducing the amount of foaming agent or increasing the mold temperature; Replacing a portion of F-11 (23.7 ℃) with high boiling foaming agent dichloromethane (39.8 ℃) can significantly increase the thickness of the epidermis; To improve the pore structure and increase the porosity, a small amount of air can be injected in a controlled manner. (Increase nucleation effect) c、 The mold temperature should be strictly controlled according to the raw materials, process, and mold conditions. (2) Advanced equipment, reasonable configuration, simple structure, excellent materials, easy operation, and simple maintenance. (3) Operators or maintenance personnel are able to regularly maintain or replace vulnerable parts as required. 3. Production process flowchart of polyurethane self skinning products
In order to increase production and save raw materials, a batch of molds should be centralized for intermittent pouring (controlled by a computer program controller). After the intermittent pouring of a batch of molds is completed, the mixing chamber of the pouring machine should be automatically cleaned. In this way, multiple self skinning products of the same or different specifications can be produced at once.
Ⅲ、 Structure Introduction: (1) Soft foam pouring machine (composed of tank, pump, head, and controller) (see PU20F-R machine flowchart for details) A、 Material tank (tank): The tank body is made of acid resistant stainless steel inner liner (argon arc welding), heating jacket, and outer polyurethane rigid foam insulation layer. The new structure adopts a flat cover processed by machine tools, which improves concentricity compared to convex covers. The mixing shaft is shorter, making mixing more stable and sealing more reliable. This reduces the space at the top of the material tank and reduces moisture inside the tank, which can cause raw materials to deteriorate. B、 Measurement section (pump): 1. Factors affecting measurement accuracy: (1) Balanced feeding and normal filtration: The viscosity of the raw material is related to the material temperature. Under the conditions permitted by the process, it is more convenient to increase the material temperature and reduce the viscosity for feeding. If the viscosity of the original solution is too high (>2000CPS), add<0.03Mpa nitrogen gas to the tank to achieve balanced feeding to the metering pump. (2) Metering pump: The structure and accuracy of the driving device and speed digital display. Due to the use of low-speed high-precision metering pump, precision driven continuously variable transmission and digital tachometer, under correct usage conditions, the error should be less than 0.5%. (3) The resistance of the feeding and reflux system is stable, and the pressure regulation is sensitive. Note: The measurement method for high demand polyurethane equipment adopts the “full reflux pouring” process instead of the “straight through” process The filtered A and B raw materials from the material tank are respectively input into the mixing device by the metering pump according to the formula requirements, and can be poured after uniform mixing. Its advantages are simple process, no need for reflux pipes, and it is commonly used in situations with low requirements, such as polyurethane rigid foam spraying. The process of “full reflux pouring”: It is transported to the mixing device by metering pumps A and B, controlled by a synchronous switch, and poured When the full amount of A and B materials enter the mixing chamber, they can be mixed evenly under the action of the high-speed mixing head before pouring; If the pouring is stopped, the A and B materials will be cut off from entering the mixing chamber, and all will flow back to the original material tank. By adjusting the feed pressure and reflux electrical pressure, a constant mixing ratio can be maintained during pouring, which will not cause changes in the mixing ratio (instantaneous ratio) at the beginning or end of mixing and result in secondary or waste products, greatly improving the yield of genuine products. 2. Metering pump configuration and main parameters: Design mixing ratio: A: B=100:40 (infinitely adjustable) (pouring time: 3~6S)
C、 Mixing device (pouring head) Pouring reflux switching device: The three cylinders switch between two components of the rotary valve shaft synchronously through the rack and gear. When the rack is in the highest position, the A and B rotary valves are in the position of air flushing or cleaning the mixing chamber, while the A and B materials are in the reflux state; When the rack is in the middle position: A and B materials are in a reflux state, and cleaning or air flushing is turned off (so the cleaning hole is never blocked); When the rack is in the lowest position: cleaning or air flushing is turned off, and materials A and B are in the pouring state. During pouring, the raw materials A and B are injected into the mixing chamber through the small holes of the throttling plate; When refluxing, the original liquid returns to each feed tank through the reflux regulating valve (to prevent the generation of bubbles and stabilize the feed temperature, the refluxed original liquid enters the feed tank from the bottom) Pressure regulating device: The reflux regulating valves installed on both sides of the pouring head can precisely adjust the reflux pressure of the original solution (requiring sensitive adjustment, reliable fine-tuning, and no blockage). The pouring pressure can be adjusted by the aperture of the throttle plate, and the aperture of the throttle plate can be determined by referring to the following formula: d(mm)=5√Q/V Q: The flow rate of the original solution (L/min) is determined based on the pouring volume. V: The flow rate of the original solution (m/s) is usually set at 3-5. Mixing transmission and shaft end sealing: The two pole motor is driven by a synchronous gear belt, with a stirring speed of 4750r/m. The bearings are imported high-precision bearings, and the shaft is equipped with precision oil seals and special seals to prevent the mixture from pouring upwards. (During operation, attention should be paid to timely replacement when the discharge port of the funnel becomes small due to material accumulation, to avoid pouring upwards due to high pressure in the mixing chamber). Cleaning device: To ensure that the mixing chamber of each batch of products is clean (without air leakage or residual cleaning solution) after pouring, in order to ensure the smooth progress of the next cycle of pouring. By using a computer program controller and an electromagnetic valve, it can automatically perform air flushing or liquid washing, and effectively prevent the original liquid from pouring into the cleaning pipeline. Mixing head: Adopting a specially designed high shear mixing head: simple and practical, uniform mixing, no pressure fluctuations during intermittent pouring, and easy to clean. Changing the size of the funnel discharge hole can adjust the residence time of the mixture in the mixing chamber. D、 Control and Display (Control) Computer programmer (stable performance, reliable structure, easy operation, easy to understand and learn) (1) Automatic control and display of pouring volume, capable of controlling different or the same pouring volume for 99 workstations (pouring time 0.10-99.9 seconds) (2) Control the braking of intermittent pouring: After each mold is poured, in order to prevent dripping of the pouring head, the gear of the rotary valve shaft should be in the middle position (original liquid reflux, cleaning closed) when the pouring stops. At this time, the mixing head motor stops and brakes. (3) Control automatic air flushing and liquid washing: After a batch of molds is poured, if the pouring is stopped for a long time (more than 2/3 of the milk white period), the automatic cleaning program should be carried out: air flushing – liquid washing – air flushing (all the above mixing heads rotate at high speed) – air flushing (mixing head stops rotating). Adjust the time of each program to clean and dry the mixing chamber. Temperature control system: The stability of material temperature is necessary to ensure normal production. Generally, a material temperature of 22 ± 2 ℃ is required. The raw liquid is heated by the electric heating tube inside the jacket at the bottom of the material tank through the heating of thermal oil. The material temperature is automatically controlled by a digital temperature controller through a temperature sensor at the bottom of the material tank. Raw liquid pressure display: Adopting high-precision digital pressure gauges and thin-film pressure sensors, the display accuracy can reach 0.01Mpa Flow (metering pump speed) display: The measurement is displayed by a high-precision tachometer. Pump speed can be calculated or measured to determine the flow rate and mixing ratio of each pump. (2) Die bearing production line: designed and manufactured according to user requirements.
Ⅳ、 Reference materials for model selection: (1) There are three processes and related equipment for the production of molded polyurethane. ① High pressure machine: using a high-pressure pump to measure, the two raw materials form a high-speed liquid flow (>150m/s) and collide and mix. The mixing chamber is scraped clean by a precision matched high-pressure push rod. Due to the use of high-pressure collision mixing and self consolidating pouring head, its advantages are that the pouring head is relatively lightweight and does not require solvent cleaning after pouring, making it suitable for production with long intervals after each pouring (such as commonly used refrigerator production). The structure of the high-pressure machine is complex, the investment is large, and the requirements for operation and maintenance technology are high. However, the high-pressure machine is not suitable for raw materials with very small pouring volume or two component mixing ratios and large viscosity differences. ② High speed machine: using medium pressure metering and high-speed serrated screw mixing (speed>15000 revolutions per minute), the mixing chamber is scraped clean by pushing the conical high-speed screw, without the need for solvent cleaning (such as DESMA machine). It requires high processing accuracy, complex mechanism, large equipment investment, and high requirements for operation and maintenance personnel. Currently, small pouring volume equipment is mainly used. ③ Low pressure machine: using low-pressure metering, mechanical stirring and mixing, and cleaning the mixing chamber with solvent. Its advantages are simple structure, easy operation, and low investment. It can be used for various viscosities or mixing ratios of raw materials, with a wide range of adjustments. It is particularly suitable for batch production of polyurethane products after pouring dozens of products (only cleaned once after pouring dozens of times) (2) Comparison of three models: Although high-voltage machines or high-speed machines have their own advantages, imported machines or imported parts assembled machines are still preferred for reliable quality. As a developing country, China is still “unable to afford and maintain”, making it difficult for users to obtain substantial benefits. Moreover, due to the weak industrial foundation in China, especially in materials, heat treatment, and precision machining, there is a significant gap compared to advanced industrial countries. Currently, although domestically produced high-voltage machines and high-speed machines are replicated, they can only achieve a “similar appearance” and cannot be “similar” to original imported machines.
Ⅴ、 Basic formula weight parts (pbw) High activity polyether polyol: hydroxyl value 25-30, Mn = 4000-6000 100 Chain extender (aromatic diamine) 0-30 Crosslinking agent (butanediol, ethylene glycol, amino polyol, diamine) 0-8 Tertiary amine catalyst 0.21.5 Tin catalyst 0.0050.025 Pigment paste/light stabilizer 3-10 Foaming agent: F-11 or dichloromethane 16-30 Foam stabilizer 12 Isocyanate
 FEILONG PU MACHINE